
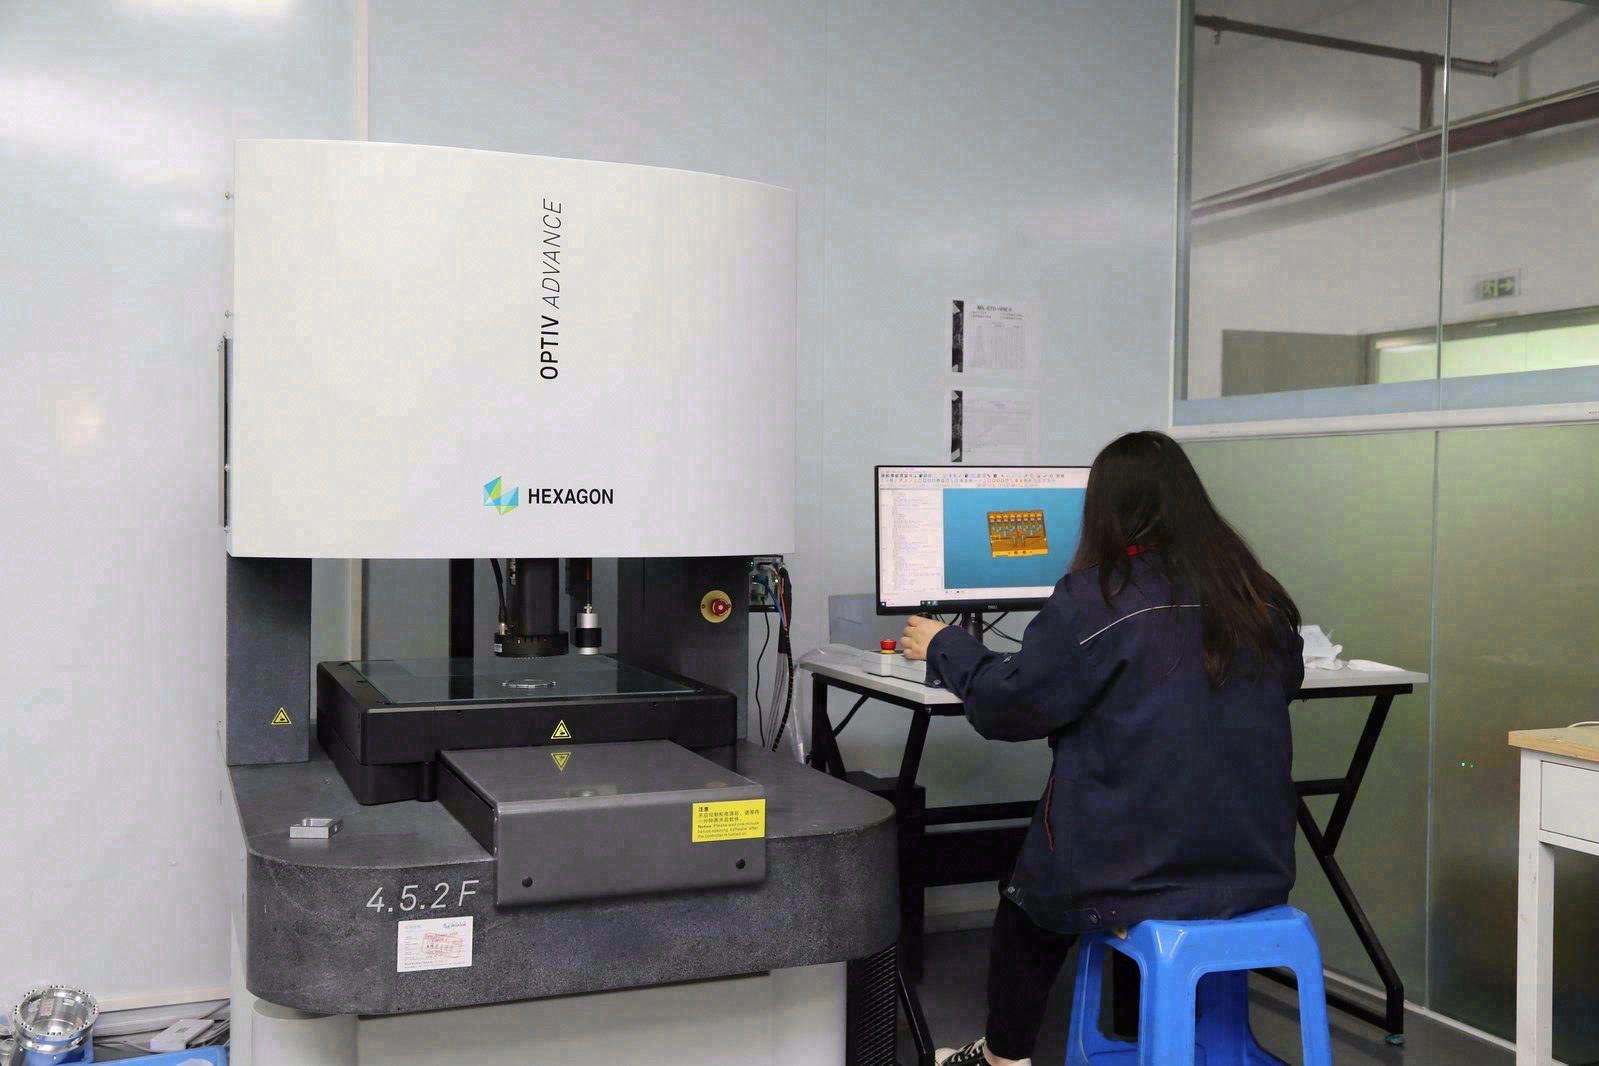
Sourcing medical parts from a Swiss CNC machining supplier is a verification exercise. The geometry is the easy part; what makes a slender implant screw or instrument pin usable is whether the material can be proven against its certificate, the roundness and tolerances held and measured, and the records assembled in a form your quality system can put into the device history record. This guide walks through the material callouts, tolerance and finish strategy, finishing chain, and documentation scope for medical Swiss-type work, and the due diligence that qualifies a supplier before the first part ships.
Why does medical sourcing turn on documentation as much as machining?
A medical component is judged by the evidence trail that surrounds it. Your quality system — and, for cleared or approved devices, the regulator — reconstructs the part's history from certificates, inspection data, and process records. A substituted alloy or an out-of-tolerance feature that passes visual inspection becomes a liability precisely because the record is what gets audited, not the part's appearance.
That shifts the buyer's standard from "can you make this?" to "how do you prove you made it correctly, every time?" Material: the alloy on the drawing must match the certificate on the bar in the machine. Geometry and finish: the size, roundness, and surface finish must be measured, not assumed. Documentation: the reports must let an engineer who was not present confirm the part months later, when the device history file is reviewed.
That due diligence sequence — entity, machines, evidence, certificates, terms — is the framework this supplier publishes, and it is covered in the Swiss machining FAQs. Medical simply raises the standard of evidence on the same process.
Which materials matter most for medical Swiss-type parts?
Medical Swiss-type machining concentrates on a narrow material set — much of it supplied as free-machining bar, because the guide bushing and bar feed work best with material that cuts cleanly — and the drawing should name the grade and specification so the certificate is matched to it:
| Material | Typical medical use | Why it is specified |
|---|---|---|
| 316L stainless | Implants, instrument pins, fasteners | Corrosion resistance, passivation response, established biocompatibility data |
| 303 stainless | Instrument fittings, slender pins | Free-machining for bar-fed Swiss production of non-implant parts |
| 17-4PH stainless | Cutting and load-bearing instruments | High strength after heat treatment for thin, hard tools |
| Ti-6Al-4V | Bone screws, implant pins, rods | Strength-to-weight and biocompatibility |
| PEEK | Radiolucent and insulating components | Machinable polymer with a long implant history |
The material callout matters twice: once for the certificate, and once for the machining strategy. Titanium and 17-4PH turn slowly on a Swiss machine and demand careful speeds; PEEK demands sharp tooling and controlled heat; 303 is specified precisely because it feeds fast and breaks chips through the guide bushing. Each changes the quote and the schedule, which is why the grade belongs on the drawing before the RFQ goes out.
What tolerances and roundness should a medical drawing carry?
Medical Swiss-type parts carry their function in the geometry of rotation — diameters, roundness, concentricity, straightness along a slender axis. Production capability on turned features is ±0.003 mm, with ±0.002 mm reachable by precision grinding on bearing and sealing surfaces, and process capability of Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window is the standard to quote and verify.
Roundness and straightness deserve their own lines on a medical drawing because a screw thread that is slightly out of round, or a pin that bows, fails in ways a size tolerance cannot see. State which diameters carry roundness and cylindricity callouts and which axes carry straightness, and confirm they will be verified on the CMM — with the slender part checked in-process while it is still supported, because it flexes under its own weight once free.
Surface finish belongs on the drawing in Ra values, because on medical parts it is functional: a fine finish on an instrument reduces friction and cleaning problems, and passivation is the step that restores corrosion resistance after machining. A finish stated as Ra 0.4 µm is one the shop can quote and verify with a profilometer; a finish described as "good" is a guess.
What documentation should a medical order require?
The documentation on a medical order is part of your device history record, so it should be scoped into the purchase order rather than requested after machining:
- Material certificates naming the alloy, temper, heat number, and the specification on the drawing.
- Incoming verification records proving each lot was checked against its certificate before cutting.
- CMM dimensional reports with roundness data on the critical diameters, measured against the drawing's datum scheme.
- Surface-finish measurements backing the stated Ra values with profilometer data.
- SPC data on key characteristics backing the Ppk ≥ 1.67 initial claim across the run.
- Finishing and process records for passivation, electropolishing, anodizing, or heat treatment.
Each document moves verification work from your incoming inspection into the supplier's routine. A supplier that ships reports as standard practice is one whose process you can audit; one that treats documentation as an extra will leave gaps in your device history record. Ask how long the supplier retains records, because your file may need them years after the shipment, and confirm the report format, because machine-readable dimensional data is far easier to load into your record than a scan.
How is material traceability handled on a medical lot?
Traceability is a chain, and it only holds when every link is documented. The chain runs: the mill certificate arrives with the bar; the incoming check verifies the lot against it — XRF spectroscopy is the standard method and catches a substituted alloy before cutting; the production record ties finished parts to the lot; and the reports ship with the order.
Ask how the shop records the chain and whether the verification record for your lot can be included with the certificates. A supplier that logs material source, machine, batch, and operator against each lot can trace a non-conformance to a specific batch — exactly what your quality system needs when a field question surfaces. One that answers "the paperwork is in a folder" does not have traceability in a usable form.
Expect the incoming check to be visible rather than assumed. A serious shop can show you the verification step and the record it generates, which is worth confirming on a live video walk-through. On a medical component, the incoming check is where a material substitution is either caught or allowed into the device history record, and it deserves the same audit attention as the machining itself.
How do finishing and cleaning fit into the medical workflow?
A medical component rarely ships as-turned. Stainless instruments and implants are passivated and often electropolished; titanium components are anodized or passivated; PEEK parts may need specific surface preparation. Each step is a documented process with its own records, and the specification should state which steps are required and what evidence accompanies them.
Ask the supplier which finishing steps run in-house and which go to a qualified partner. A shop that manages the chain can deliver a finished, documented component from one accountable source; a split across vendors splits the records and the accountability. Cleanliness requirements — whether the part ships clean, in controlled packaging, or with a final cleaning step documented — belong in the specification, not in a conversation after quoting.
Consider whether your program needs the finish process itself validated. A passivation bath or an electropolish cycle is only as good as its control, so ask what records the supplier keeps on the finishing process — cycle parameters, and the inspection that confirms the result on your lot. On a regulated component, the finish is part of the specification, and its evidence belongs in the device history record alongside the machining data.
Which quality systems should a medical supplier hold?
Match the certificate to your program requirement rather than collecting an impressive list. Many medical device manufacturers require component suppliers to hold ISO 13485 or to operate under the manufacturer's own quality system — where your supplier quality agreement demands ISO 13485, only a holder will pass your audit. For build-to-print work under your system, a supplier certified to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015 provides an audited structure for document control and traceability that the device history record runs on.
Verify the numbers, not the logos. Every certificate carries a registrar reference, and a lookup confirms it is current, in the correct legal name, and scoped to what the supplier claims. Read the scope line as carefully as the standard itself: a scope that excludes product design confirms the shop is build-to-print, which is the arrangement that keeps design responsibility with your organization, where the regulator expects it.
Certificate checks are one layer of a supplier audit that also covers the machines, quality evidence, and a live floor walk. The full sequence is the due-diligence framework this supplier publishes, and it applies to any supplier you evaluate for a regulated program.
How do you run due diligence on a medical Swiss machining supplier?
The buyer due-diligence framework that protects a regulated program runs in five steps, in order:
- Confirm the legal entity. Ask for the legal name and registration number and verify them against a public registry.
- Verify the machines. Ask for the machine list — including the Swiss-type bar envelope — and reconcile it against the floor on a visit or live video walk.
- Check the quality evidence. A CMM report with roundness data from a real job, not a capability statement.
- Verify the certificates. ISO 9001:2015, IATF 16949:2016, and ISO 14001:2015 with numbers you can check with the registrar, in the same legal name.
- Agree the terms and validate with one part. Order at a 1-piece MOQ, measure the first article against the drawing, and review the documentation before releasing volume.
Each step removes an unknown before the next, more expensive step. Qualification is not a one-time event — re-run the framework when the program changes, and treat the first article of every new part as a qualification event in its own right. Re-qualify on a schedule too: a yearly certificate check, a re-run sample when the process changes, and a standing notification requirement for material-source changes, because on a regulated component the supplier's change control is part of your change control.
What are realistic timelines and order structures for medical work?
Medical Swiss machining runs on two rhythms. Prototypes and first articles are urgent and small: with a 1-piece MOQ, a single slender part can be machined, verified against its material file and CMM report, and approved before volume is committed. Production orders are larger and slower, gated by first-article approval and carrying per-lot inspection and documentation.
On the calendar, simple pins typically ship in about a week, while parts with many operations, grinding steps, or finishing chains run three to six weeks once inspection and documentation are counted. The shipping leg is separate again: fly prototypes so the design loop is measured in days, let production quantities ride ocean freight, and book logistics in parallel with machining rather than after it. Lead times from a Swiss supplier follow the 3 / 7 / 30-day ladder by process-step count.
Keep the documentation standard identical across both stages. If your quality system needs CMM reports, roundness data, finish measurements, and certificates on the prototype, it needs the same on every production lot, and building the habit at prototype stage means the device history record is never assembled from missing documents later. The part types that suit each stage are on the parts guide.
Frequently Asked Questions
Which materials are most common for medical parts made by Swiss CNC machining?
The core set is 316L stainless for implants and instruments, 17-4PH stainless for cutting and load-bearing instruments, Ti-6Al-4V for implants and weight-critical components, and PEEK for radiolucent parts. Small slender components also use 303 where free machining matters. The finishing steps matter as much as the alloy.
What tolerances and roundness should a medical drawing carry?
Production capability on turned features is ±0.003 mm, with ±0.002 mm reachable by precision grinding on bearing and sealing surfaces. Roundness on critical diameters is verified on the CMM, and slender geometry is checked in-process while supported. Process capability of Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window is the standard to quote.
What documentation should a medical order require from a Swiss CNC machining supplier?
At minimum, the material certificate and a CMM dimensional report with roundness data on critical diameters. For a device program, add incoming verification records, SPC data on key characteristics, and a first-article report. The documentation is part of your device history record, so scope it into the quote.
Does a Swiss CNC machining supplier need ISO 13485 for medical work?
It depends on your program. Many medical device manufacturers require component suppliers to hold ISO 13485 or to operate under the manufacturer's quality system. Where your supplier quality agreement requires it, only an ISO 13485 holder will pass. For build-to-print work under your system, a supplier certified to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015 can still deliver the traceability and inspection documentation the part needs.
How is material traceability handled on a medical lot?
Every incoming lot is checked against its mill certificate before cutting, typically by XRF, and the certificate travels with the finished parts. The chain — certificate, incoming check, production record, shipped reports — is what lets your quality system trace a lot into the device history record.
How do finishing and cleaning fit the medical workflow?
Passivation and electropolishing of stainless, anodizing of titanium, and PEEK surface prep are documented steps. Cleanliness requirements belong in the specification, and the supplier should state which steps run in-house versus with a qualified partner. Finish is verified with a profilometer, not assumed.
How do I run due diligence on a Swiss CNC machining supplier for medical work?
Confirm the legal entity, verify the machines, check the quality evidence, verify the certificates, and agree the terms. Then order one part at a 1-piece MOQ, measure it against the drawing, and review the documentation before releasing volume.
How do I keep quality consistent from prototype to production?
Release in stages: approve the prototype's material file and CMM report, then run a pilot batch carrying its own first-article report and SPC data on key characteristics. When the same machines and programs produce both, the approved geometry is repeated rather than re-derived.
Have a medical drawing to qualify?
Email the model, the toleranced drawing, and the material callout to [email protected] or call +86 13126536955. You will get the due-diligence evidence in writing, a DFM review, and an itemized quote — usually within one business day.